
Knorr-Bremse’s Begins Construction Of EUR 200 Million Chennai Future Campus
- By MT Bureau
- February 15, 2026
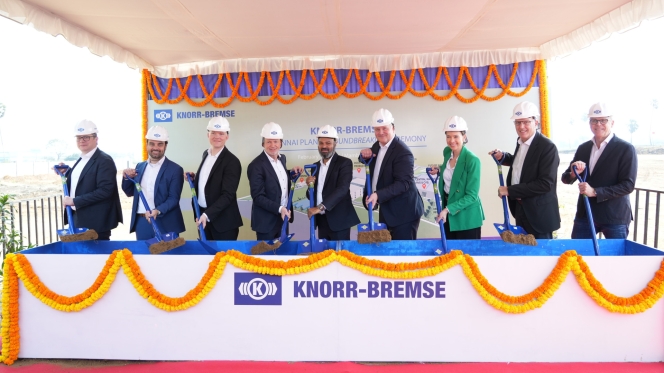
Groundbreaking for innovation, growth and customer focus – Knorr-Bremse launches its modular campus in Chennai. Also attending: Executive Board member Rail, Dr. Nicolas Lange (fourth from left), and members of senior management.
German component manufacturer Knorr-Bremse has initiated the construction of a modular campus in Chennai, India, with an investment plan of up to EUR 200 million over the next five years. The facility will integrate engineering, production and artificial intelligence (AI) activities.
Scheduled to commence operations in late 2027, the site will support both the Rail and Truck divisions. The campus is designed to accommodate up to 3,500 employees and will complement existing sites in Pune and Palwal.
The 188,000 square metre facility will be developed in phases. The initial stage includes production plants for metro and high-speed train entrance systems, alongside braking components for commercial vehicles. Later phases, extending to 2030, will add office complexes to house global business services, including finance and HR functions.
Products manufactured at the Chennai hub are intended for the Indian domestic market and global exports. Knorr-Bremse is currently a supplier for rail projects in Delhi and Chennai and is providing braking and sanitation systems for India’s high-speed rail network.
The company selected Chennai due to its infrastructure and engineering landscape. The new campus is located near the Knorr-Bremse AI centre established in 2025. This proximity is intended to accelerate digital projects and improve process efficiency.
Marc Llistosella, CEO, Knorr-Bremse, said, “India is a key region for us with great potential – as a location for innovation, a production hub, and a transport market. Our future campus enables us to connect global capabilities even more closely, make processes more efficient, and accelerate projects. This creates a strong foundation for our Rail and Truck divisions to grow profitably – in India as well as in international markets. The campus is an important building block in our global strategy and a clear commitment to Knorr-Bremse’s long-term growth path.”
- Stellantis
- Stellantis India
- Citroen
- Jeep
- Hindustan Motor Finance Corporation
- CK Birla Group
- Stellantis Automobiles India
- Shailesh Hazela
Stellantis Takes Full Ownership Of Thiruvallur Manufacturing Plant In Tamil Nadu
- By MT Bureau
- September 21, 2026
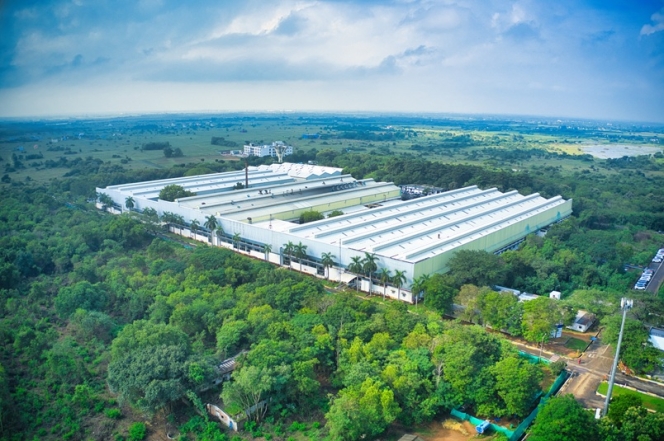
European automotive major Stellantis India has acquired the remaining equity stake held by Hindustan Motor Finance Corporation, a CK Birla Group company, in Stellantis Automobiles India. The transaction gives Stellantis complete ownership of the entity and its manufacturing facility located in Thiruvallur, Tamil Nadu.
The acquisition was funded through foreign direct investment and consolidates the manufacturing partnership established between Stellantis and the CK Birla Group in 2017.
The vehicle assembly at the Thiruvallur site began in 2021 and the plant currently produces the Citroen C3, e-C3, C3 Aircross and Basalt models. The company claims a localisation level of over 95 percent in its range.
Stellantis has allocated more than EUR 1 billion (approximately INR 110 billion) toward its Indian operations, covering manufacturing, engineering, supplier development and exports.
The automaker plans to increase annual production at the Thiruvallur facility from 16,000 units in 2026 to more than 43,000 units by 2028. The expansion is projected to increase direct site employment from 610 workers in 2026 to more than double that figure by 2028, alongside additional job creation in local supplier and logistics operations. Vehicles assembled at the plant are distributed domestically and exported to eight international markets across four continents.
Shailesh Hazela, CEO and Managing Director, Stellantis India, said, "India remains a key pillar of Stellantis' growth strategy. Having invested close to INR 110 billion in the country to build a strong manufacturing, engineering and export ecosystem, we continue to see significant opportunities ahead. This milestone will enable greater integration and enhance our ability to respond more quickly to customer and market needs."
"As we look ahead, we are committed to driving growth through new product investments, expanded manufacturing capacity, stronger export competitiveness and deeper localisation. India is playing an increasingly important role within Stellantis' global network, and we see significant potential to further scale our operations and contribution to the country's industrial growth," Hazela added.
The buyout removes the joint venture structure, establishing direct operational control for Stellantis to align Indian manufacturing capacity and export distribution with its central corporate operations.
- Audi AG
- Audi A2 e-tron
- Ingolstadt
- Audi A3
- Gernot Dollner
- Jorg Schlagbauer
- Gerd Walker
- Siegfried Schmidtner
Audi Commences Production of A2 e-tron At Ingolstadt Plant
- By MT Bureau
- September 11, 2026

German automotive luxury brand Audi has started series production of the all-electric A2 e-tron at its main plant in Ingolstadt, Germany.
Interestingly, the company claims that the development timeline for the A2 e-tron was reduced by 21 months compared to previous vehicle projects through streamlined pre-series evaluation and coordination processes. The EV manufacturing process incorporates structural changes to lower operational complexity.
Audi implemented the string-of-pearls production sequence at Ingolstadt, fixing customer order sequences six days prior to assembly. This system allows component suppliers to deliver pre-sorted parts directly to the assembly line, eliminating regional storage and component sequencing areas.
The body of the A2 e-tron is assembled on shared line infrastructure alongside the Audi A3, utilising more than 1,200 reallocated components and 250 repurposed welding robots. Automated systems include camera-guided bin-picking robots for small sheet-metal parts and fully automated wheel installation stations replacing semi-automated bolting in chassis preassembly.
On the digital infrastructure side, the plant runs the Edge Cloud 4 Production platform, which centralises the control units for vehicle commissioning and operator guidance systems, replacing over 450 industrial PCs in the assembly area.
The facility also uses artificial intelligence assistants, including supply chain and maintenance chatbots, to assist line personnel with fault diagnostics and documentation retrieval.
Gernot Dollner, CEO, Audi AG, said. "The Audi A2 e-tron represents the next step in our renewal. It shows how we consistently think from the market backward, because different regions need different answers. The A2 e-tron was developed for Europe and is manufactured in Ingolstadt. It is the most efficient Audi we have ever built, and it makes electric mobility suitable for everyday use. At the same time, it shows how we are implementing our transformation in concrete terms: developing faster, producing more efficiently, and thereby strengthening industrial value creation and competitiveness in Germany."
Jorg Schlagbauer, Chairman, Audi General Works Council, said, "The start of production of the A2 e-tron in Ingolstadt is a strong signal for our site and its future. We are particularly proud of this as the works council, because together with the workforce we have repeatedly fought with great determination since 2019 for Audi to develop an entry-level electric model and build it in Ingolstadt. The project stands for technological expertise, industrial value creation, and secure prospects for our employees. Above all, however, the successful production launch is the result of the tremendous commitment and skill of our colleagues. Once again, this shows: at Audi, Vorsprung durch Technik is not just announced, it is achieved."
Gerd Walker, Board Member for Production and Logistics, Audi, said, "The A2 e-tron again demonstrates that it is possible to build cars profitably in Germany. Particularly important in this regard are AI assistants developed jointly by our Neckarsulm and Ingolstadt sites, our highly flexible production facilities, and, above all, the expertise of our employees. The model demonstrates the transformation of Audi production: less complex, even more efficient, and with a high degree of digitalisation and automation."
Siegfried Schmidtner, Plant Manager at Audi Ingolstadt, said, "The start of production of the Audi A2 e-tron is the result of extensive teamwork at the Ingolstadt plant. Drawing on their wealth of experience from numerous product launches, the team has laid the groundwork for a successful ramp-up of the model and further optimised our processes. Production of the new model strengthens core capabilities at our headquarters."
The site prepared its workforce for the launch through a multi-stage qualification program combining traditional assembly line instruction with virtual reality training modules.
LICO Partners Epsilon Advanced Materials For Battery-Grade Graphite Recovery
- By MT Bureau
- September 10, 2026
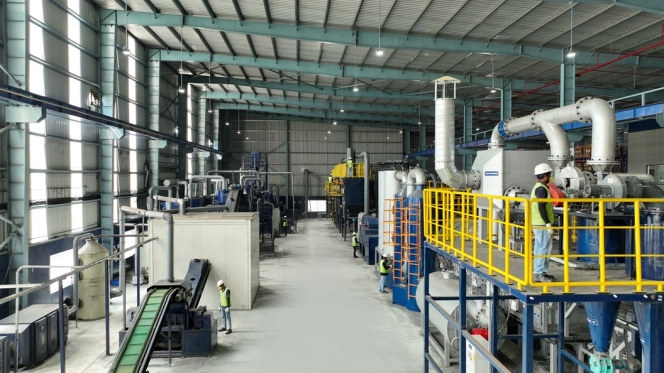
LICO Materials and Epsilon Advanced Materials have established a supply agreement to recover graphite from end-of-life lithium-ion batteries and cell manufacturing scrap for use as secondary feedstock in battery anode production.
Under the partnership, LICO Materials will process battery waste and manufacturing scrap using its mineral recovery technology to isolate graphite. The material will be supplied to Epsilon Advanced Materials for qualification and integration into its synthetic, natural, and blended graphite anode production platforms. Product samples from the recovered feedstock will be distributed for customer testing by the end of 2026. Graphite constitutes 20 to 30 percent of a lithium-ion battery's weight.
At present, China controls over 90 percent of global graphite refining and anode material production, with International Energy Agency projections indicating China will supply 80 percent of battery-grade graphite through 2035. India's Ministry of Heavy Industries projects domestic lithium-ion battery demand to reach 210 gigawatt-hours by 2030, requiring 200,000 to 230,000 tonnes of graphite anode material annually.
Gaurav Dolwani, CEO and Founder, LICO Materials, said, "Graphite is a critical material for the battery industry, yet its supply chain remains highly concentrated in China. Recovered graphite gives us an opportunity to retain material that is already within the battery ecosystem and return it to productive use. Supplying this recovered graphite to Epsilon Advanced Materials marks a breakthrough in our journey beyond battery recycling and brings us closer to closing the graphite loop."
Vikram Handa, MD, Epsilon Advanced Materials, said, "As global battery manufacturing expands, diversifying sources of graphite has become increasingly important. Recovered graphite provides an opportunity to complement conventional feedstocks while retaining valuable material within the battery ecosystem. Our work with LICO creates a pathway to bring recovered graphite back into advanced anode material production and strengthens the circularity of the battery materials value chain."
The agreement establishes domestic secondary feedstock sourcing for battery anode production, reducing reliance on primary graphite imports as Indian battery cell manufacturing expands.
Ultraviolette To Build 250,000 Units Per Annum Capacity BIGGA Factory In Hosur
- By MT Bureau
- September 10, 2026
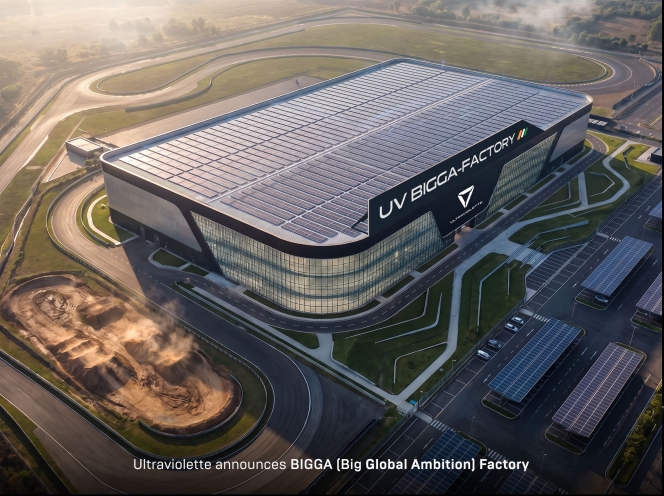
Bengaluru-based electric vehicle maker Ultraviolette Automotive has announced plans to establish a new manufacturing facility – the BIGGA Factory – in Hosur, Tamil Nadu. The plant will manufacture the Tesseract electric scooter and support the company's future product portfolio across sports, crossover, cruiser and street motorcycle segments.
The facility, located at the SIPCOT Industrial Park in Shoolagiri, will feature an initial production capacity of 250,000 units per year, which can be scaled up to 500,000 vehicles annually.
The site will complement Ultraviolette's existing plant in Bengaluru, Karnataka. The project is expected to generate approximately 2,000 jobs during its first phase.
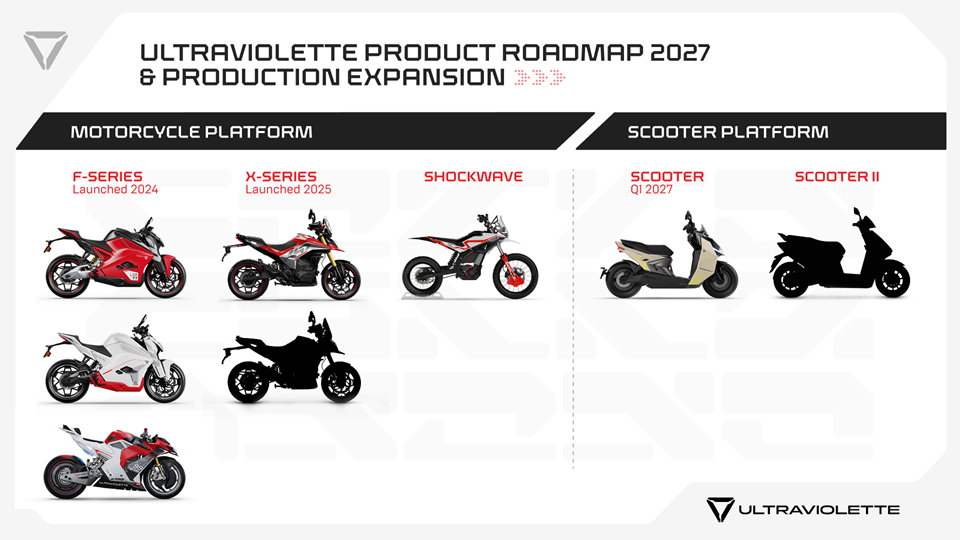
The manufacturing setup will integrate Industry 4.0 systems, a Manufacturing Execution System for real-time tracking, collaborative robots for welding and assembly and vision-based inspection tools. The facility will also include an on-site test track to evaluate completed vehicles prior to delivery.
Narayan Subramaniam, Co-Founder and CEO, Ultraviolette Automotive, said, "We are at an inflection point in Ultraviolette's journey. Over the last few years, we have built our foundation around technology, performance and product innovation; the next phase is about building the scale to take that foundation much further. The BIGGA Factory is a significant step in that direction, giving us the manufacturing capacity and infrastructure to scale Tesseract and our future products, while creating the ability to serve a much larger customer base in India and international markets. Our current facility in Bengaluru, Karnataka will continue its regular operations alongside the BIGGA Factory, strengthening our long-term manufacturing and technology footprint in India."
Niraj Rajmohan, Co-Founder and CTO, Ultraviolette Automotive, said, "Hosur is a key manufacturing hub with a well-established automotive ecosystem, significant supply-chain advantages and close proximity to Ultraviolette's R&D operations and existing supplier network. These strategic advantages, combined with the scale, precision and manufacturing agility of the BIGGA Factory, will enable us to deliver the Tesseract and our future products to customers in India and international markets while maintaining the highest standards of quality and performance. The BIGGA Factory will further strengthen our ability to innovate and contribute to India's emergence as a global hub for electric-vehicle technology and manufacturing."
Comments (0)
ADD COMMENT