

Witnessing manufacturing modernisation since Maruti Udyog began producing cars in collaboration with Suzuki of Japan at Gurgaon in 1984, the Indian auto industry landscape has drastically changed. Opening up to automation with the installation of some of the best robots available at Kuka, ABB and others, the auto industry has left no stone unturned. Such has been the fervor that Tal, a Tata Motors company, launched a robot called Brabo in 2018 to make manufacturing processes involving the application of sealants, picking and placing of parts, welding and vision inspection reliable and easy to perform. Made with an eye on manufacturing process the world over, the Brabo was tested in over 50 work streams and has so far found use in sectors like lighting, aerospace, software, electronics, plastics, education and logistics sectors apart from the auto industry. Coming from an auto maker that installed 300 Kuka robots to automate the assembly of Sumo and Safari at its Pune plant in 2009, the Brabo has seen many rounds of development and application-preparedness since its launch.
Smart manufacturing trend
Highlighting the smart manufacturing trend, the TAL Brabo robot with payloads of two and 10 kilos has also found favour with companies in Europe and other places. Highlighting the prowess of Artificial Intelligence (AI) and Internet of Things (IoT), the robot is an example of the fast-changing manufacturing canvas. Producing about 1,286 engines per day, the Igatpuri plant of Mahindra & Mahindra became India's first carbon-neutral manufacturing facility by adopting smart manufacturing practices under Industry 4.0 in 2019. It invested in energy efficient technologies among others. It invested in recycling of water and other waste. It invested in solar panels to power some of its processes in the plant. An industry source expressed that the rapidly changing business environment the world over is providing impetus to smart manufacturing. It is driving efficiency enhancements and collaborations, he added. Emphasising on efficiency enhancements and collaborative efforts as key smart manufacturing drivers, an industry expert stated that technologies like AI, Industrial Internet of Things (IIoT), automation, big data and 5G are the biggest triggers. They are touching every aspect of manufacturing, from sourcing of raw materials to final inspection, he quipped.

Industry 4.0
As companies like Lincode (it has collaborated with Switzerland-based Global Automotive Alliance), specialising in AI-powered visual inspection with multiple patent-pending defect detection capabilities, find more and more takers in India, the smart manufacturing shift is continuing to take place despite disruptions. It has, in fact, gained speed in India with the race to successfully accomplish BS VI transition in the last few years. A source in the auto industry mentioned that BS VI transition led to manufacturers upping their global ambitions. Vinay Raghunath, Partner and Leader, Automotive Sector, EY India, averred in a report that automotive shop floors are evolving and adopting digital technologies. This, he added, is happening amid challenges like slowdown in demand, non-availability of labour, concerns on health and safety management on the shop floor. Witnessing disruptions relating to ROI among other factors, as Raghunath has informed, the Indian auto industry has been an early adopter of digital manufacturing techniques.
Working to dial higher efficiency, expertise and superior productivity, the Indian auto industry has been overhauling existing assembly lines, erecting new ones and extensively re-evaluating its manufacturing processes and practices in view of smart manufacturing, especially from an automotive value chain point of view. Taking to Industry 4.0, it is leveraging AI and IoT-based manufacturing technologies to automate further – to engage in machine-to-machine communication (M2M) such that there is self-monitoring as well as self-diagnosing. Taking to Industry 4.0 to tackle unanticipated disruptions like the Covid-19 pandemic, which has put well-oiled supply chains and production lines to the test and made it painfully clear that they in their current form are not as agile or resilient as expected, the auto industry is shifting to smart manufacturing in a big way. It is exploring and experimenting; it is finding new ways. It is doing so as it absorbs a significant change in technologies and products like electrification and EVs.
Operator 4.0 and hyper-intelligence
Investing heavily in data analytics infrastructure and capabilities, the auto industry is leveraging opportunities to digitally transform itself. It is defining the boundaries of physics for data-driven model. It is focusing on digital skills development. It is supporting the rise of Operator 4.0. Taking to collaborative robots that coexist with humans in a workplace, it is transforming its ways of manufacturing significantly. Drawing attention to the semi-conductor shortage and how the auto industry was affected despite using only 10 percent of the production, Vipin Sondhi, Managing Director, Ashok Leyland, explained that the rapidly changing consumer psyche is dictating a move to a completely different technological aspect. Emphasising on material technology, he said smart manufacturing is about digitising and achieving cost competitiveness. It was some two to three years ago that the Chennai-based CV maker began implementing smart manufacturing technologies to mitigate challenges. It took to modernising and digitising existing workplaces to address quality issues that are difficult for human beings to detect and acquire made-to-order or mass customisation capabilities. It took to equipping itself with an ability to expand and contract in tandem with the market conditions even as it took to modularisation of product lines.
Automating its cab panel pressing plant at Hosur in 2019, which increased the output by up to 66 percent, Ashok Leyland has been one of the many automotive OEMs globally that are investing in hyper-intelligent automation. A confluence of AI and Robotic Process Automation (RPA), hyper-intelligent automation is redefining not just Industry 4.0 but also Operator 4.0. It is facing challenges like the high initial acquisition cost in terms of tools, but that isn’t worrying players involved like Tata Consultancy Services, Wipro, Mitsubishi Electric Corporation, Catalytic Inc and Infosys Limited among others. Estimated to grow at a CAGR of 18.9 percent as manufacturers strive to reduce energy consumption, up quality and reliability, and control costs through predictability and data-driven unique insights, hyper-intelligent automation is turning out to be yet another finer aspect of smart manufacturing. It is proving to be a big enabler for automating repetitive tasks – to enhance efficiencies, to take to cloud computing to ensure significantly more flexibility and to achieve scalability and the ability to collaborate and reduce costs.

Increasing visibility, predictability and enhancing control on operations and inventory, hyper-intelligent automation is aiding effective decision-making. Supported by development of new technologies such as 5G, which according to a domain expert, promises the need for speed and flexibility along with the capability to eliminate network instability or downtime, hyper-intelligent automation is helping automotive suppliers like Rane Madras Limited to make efficiency, reliability and cost control gains. In 2018, the company adopted automated solutions of Mistubishi Electric Corporation for its new plant in Gujarat. It led to a significant decrease in energy consumption. Aiding smart manufacturing, technologies like hyper-intelligent automation and 5G are helping the auto industry to achieve resilience and immunity against future uncertainties. They are helping to integrate Information Technology (IT) systems used for data-centric computing with Operational Technology (OT) systems – for data readiness and cyber security, and for the development of digital talent. Technologies like hyper-intelligent automation and 5G are helping to develop cross-functional profiles like engineering-manufacturing, manufacturing-maintenance and safety-security.
Tackling disruptions and smart working environment
Looking at productivity gains, emerging competition and risk aversity in the globalised world as per the EY report, the auto industry is taking to smart manufacturing to achieve significant technology transformations like electromobility as well. Apart from the creation of a smart working environment, it is also looking at the use of new materials, new process guidelines and practices. With health also becoming a disruptive factor in recent times, the auto industry is looking at automation in processes like inbound logistics, production planning, sourcing, press shop, body shop, paint shop, quality control and outbound logistics through data visualisation. With sensors and analytics shaping up, the smart working environment in a factory is coming to include AI-based alerts and fully automated work floors. This is increasingly getting compounded by data collection, historical data and high-quality extensive data mining. Helping to guarantee ROI, smart manufacturing is helping to lower the ‘takt’ time. It is also ironically undermining the involvement of humans on the shop floor.
Reducing the cost of computation, storage and connectivity, smart manufacturing is coming of age with plummeting prices of sensors, 3D printers and robots. Empowering cloud-based manufacturing techniques and a gradual increase in the understanding of emerging technologies, smart manufacturing is providing an advantage in terms of the ability to respond to market changes quickly. Taking to develop a new light-duty truck platform with export ambitions and flexibility in terms of left-hand drive and right-hand drive orientation, VE Commercial Vehicles Ltd took to automating its welding line with robots at its Pithampur plant. It also took to robotising its windshield pasting station among others. Experiencing quality, consistency, efficiency and cost gains, the CV maker is also known to have reduced the takt time and energy consumption. As global ambitions and modularity strike in view of the ability to explore new export markets with a cost competitive BS VI product, the auto industry in India is using embedded sensors, RFID and GPS etc. for smart tracking. It is using smart manufacturing technologies to monitor parameters like temperature, pressure, vibration, machine rpm and flow rate.

Smart flexibility
As part of a shift to smart manufacturing, automakers and suppliers are resorting to flexible manufacturing and AR-based solutions to upskill. They are, in view of the technologies like connected vehicles and EVs, stressing on re-aligning their traditional manufacturing setups with that of the future. Emphasising on quality, resource optimisation, streamlining of business processes and adoption of new emerging technologies, they are closely evaluating the advantages of solutions like digital twins and rapid prototyping using additive manufacturing offer. With ROI on their mind, they are embracing smart manufacturing to move up the value chain.
- Idemitsu Lube India Pvt Ltd
- Honda BB Racing
- partner
- Season 3
- Indian Supercross Racing League (ISRL)
- Japanese brands
- Indian
- racing
- lubricant formulations
Idemitsu Lubricants Strengthens Its Motorsport Presence In India With Honda BB Racing
- By MT Bureau
- November 19, 2026
Idemitsu Lube India Pvt Ltd has joined Honda BB Racing as its ‘Powered By’ partner for Season 3 of the Indian Supercross Racing League (ISRL). The partnership brings together two pioneering Japanese brands and an ambitious Indian racing team backed by lubricant formulations tailored to the extreme engine demands of the ISRL competition.
The deal follows Honda Motorcycle & Scooter India’s announcement as title sponsor of the BB Racing team, which will race on the Honda CRF450R and CRF250R in Season 3. With Idemitsu on board, the team carries the same Honda–Idemitsu combination that runs on Asia’s road-racing grids across Moto3, Moto2 and MotoGP. The partnership also adds another global name to the ISRL, as the league grows into a destination for international athletes and partners across the supercross world.
“Idemitsu has over a century of engineering experience and Supercross is one the most demanding tests of an engine and lubrications, making it a natural fit for our brand as we looking to push our boundaries. Our association with Honda BB Racing brings Idemitsu closer to India’s athletes and fans, and we are excited to be part of the team’s journey in Season 3,” mentioned Toshiya Namigishi, MD, Idemitsu Lube India Pvt. Ltd, regarding the development.
Elaborating on the association with Idemitsu Lubricants, Atul Chordia, Team Owner, Honda BB Racing said, “Building a competitive team requires the right partnerships and a shared commitment to excellence. Having Idemitsu Lubricants as our ‘Powered By’ sponsor further strengthens our vision for Honda BB Racing. Idemitsu’s legacy in engineering and lubricants brings valuable expertise to the team, and we look forward to building on this association as we compete at the highest level in Season 3. Partnerships like these are not just important for our team, but also for the continued growth of Supercross and motorsport in India.”
Eeshan Lokhande, Director, Indian Supercross Racing League, further added “Idemitsu’s partnership with an ISRL team for the upcoming season speaks volumes about the direction in which Supercross is heading. This association with Honda BB Racing is a meaningful addition for the league, showcasing how global brands value being part of Indian Supercross. We believe partnerships like this will strengthen the sport’s ecosystem and help establish India as a credible destination for Supercross on the international stage.”
With the auction for Season 3 recently concluded, franchises have locked in their line-ups of international and Indian riders, and the focus now shifts to the track. Honda BB Racing, powered by Idemitsu, will be among the six franchises looking to make an early statement when the season gets underway this December.
- ePlane Company
- IIT Madras incubation
- select
- LYNX MOSA.ic
- mixed-criticality software platform
- mission computing
- e200X eVTOL
- eVTOL Show
- USA
ePlane Company Selects LYNX MOSA.ic To Run Mixed Criticality Software Side by Side On The e200X eVTOL
- By MT Bureau
- November 19, 2026
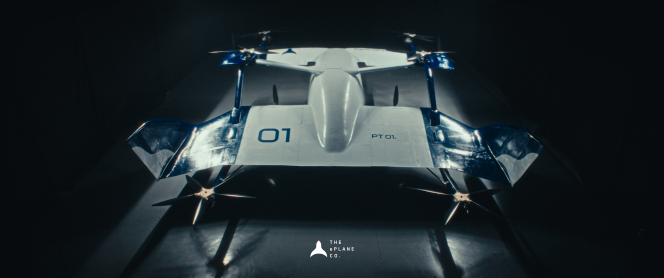
ePlane Company, an IIT Madras incubation, has selected LYNX MOSA.ic as the mixed-criticality software platform for mission computing on its e200X eVTOL. Lynx is well regarded as a leading player in safe and secure software platforms for mission-critical edge systems. The announcement was done at the eVTOL Show (USA), recently.
The e200X is a three-seat (pilot + 2 passengers) lift and cruise eVTOL with a modular airframe designed for air ambulance, urban cargo, and passenger service. Each variant carries a different payload, sensor set, and software stack, while flight control stays deterministic and certifiable in every configuration.
LYNX MOSA.ic partitions the e200X’s onboard compute so flight-critical software, such as the vehicle and energy management systems, runs in ARINC 653 partitions, isolated from lower-criticality mission functions that handle sensor data processing and situational awareness inference. Heavy AI processing runs on a separate platform, and the mission system supplies the controlled interfaces between that platform and the rest of the aircraft, ensuring clear cybersecurity and safety isolation.
“A multi-role aircraft asks more of its computers than a single-mission design, because the mission software keeps changing while flight control cannot,” said Tim Reed, Chief Executive Officer of Lynx. “LYNX MOSA.ic lets ePlane keep flight-critical software isolated and certifiable while its pilot assist software evolves with each role,” he added.
LYNX MOSA.ic is a mixed-criticality operating environment built around a separation kernel-based type 1 hypervisor. It gives each software subject its own space and time partition, so applications at different levels of criticality can share one platform, and it is certifiable to DO-178C DAL A.
"Urban air mobility is as much a computational challenge as it is an aerodynamic one. Operating high-density routes safely across emergency response, logistics, and passenger transit requires mission computing that is both certifiably safe and functionally modular. LYNX MOSA.ic gives us the deterministic partitioning required to isolate safety-critical systems while our engineers build cutting-edge aircraft functionalities on familiar tools. It is a foundational technology for delivering scalable, multi-role electric aviation," averred Professor Satya Chakravarthy, Founder and Technical Lead, The ePlane Company
Sofico Launches Sofico Intelligence, A Proactive AI And Agentic Automation Platform
- By MT Bureau
- November 19, 2026
Sofico has launched Sofico Intelligence, a dedicated artificial intelligence (AI) division that would aim to helps automotive financiers and leasing companies to spot risks and opportunities across their contract portfolios early enough to act on them and automate much of the work that would follow.
The division has been set up after Sofico acquired US-based automotive AI specialist Vinli. It has combined Vinli's agentic AI capabilities with Sofico’s experience in automotive finance and leasing, and its first focus is contract intelligence.
Sofico Intelligence is being built into Sofico Miles Enterprise, the contract management platform that already holds more than five million automotive finance and leasing contracts worldwide. Because it works inside the system that holds the contract, every change, whether it starts with an AI recommendation, a team member or a CRM, is calculated by Miles itself using the customer's own products, pricing and business rules. A person approves each change, and every step is recorded.
DENZA BAO 5 SUV Proves Its Mettle By Towing Boeing 747 ‘Jumbo’ On Only Two Wheels
- By MT Bureau
- November 18, 2026
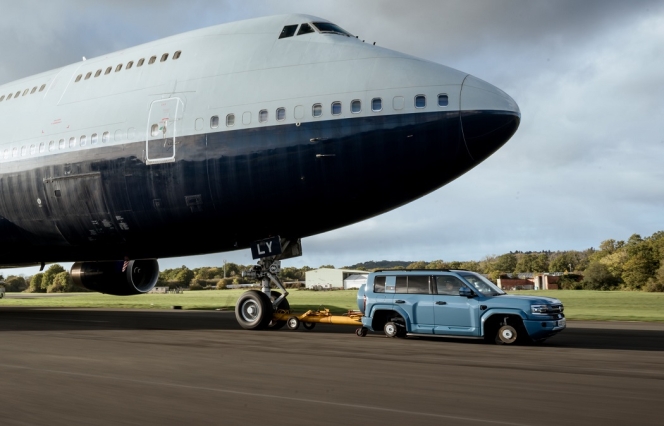
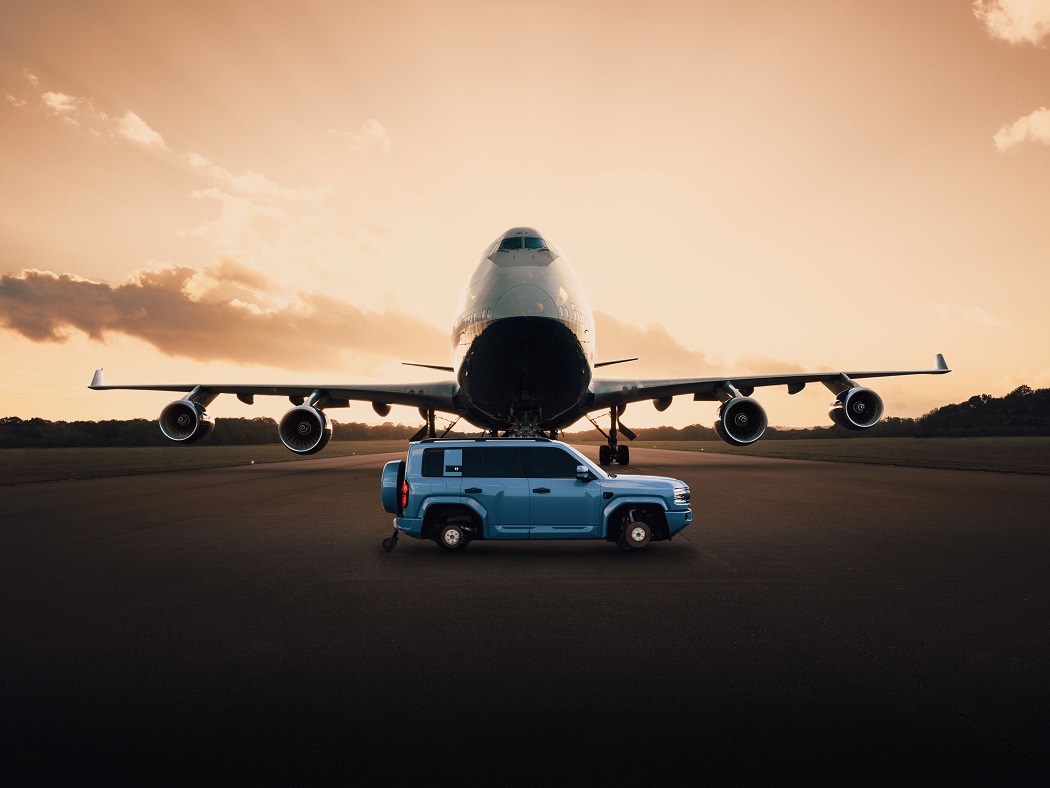
DENZA, BYD Group's premium technology-focused marque, has pulled off an impressive feat by hauling a Boeing 747 with its new BAO 5 SUV in the UK using only two driven wheels. The rugged off-roader became the first production car to tow a plane on two wheels and the first to move a 747 on electric power alone. Engineers had already set a high bar by planning to shift a 180-tonne aircraft on all four wheels, yet chose to go further still.
That drive to push limits reflects the wider BYD Group, which counts 120,000 engineers and produces more than 40 patents daily. The team attempted something entirely unprecedented to test the advanced DMO (Dual Mode Off-road) plug-in hybrid powertrain. At Surrey's Dunsfold Aerodrome, the SUV completed three runs – four wheels, then three, then two. Including pauses for filming and wheel changes, the BAO 5 covered 1,600 metres in total, or four laps of a standard athletics track. BYD UK senior technician Mark Gallifant was at the wheel, beating his earlier record of towing a fully laden double-decker bus.
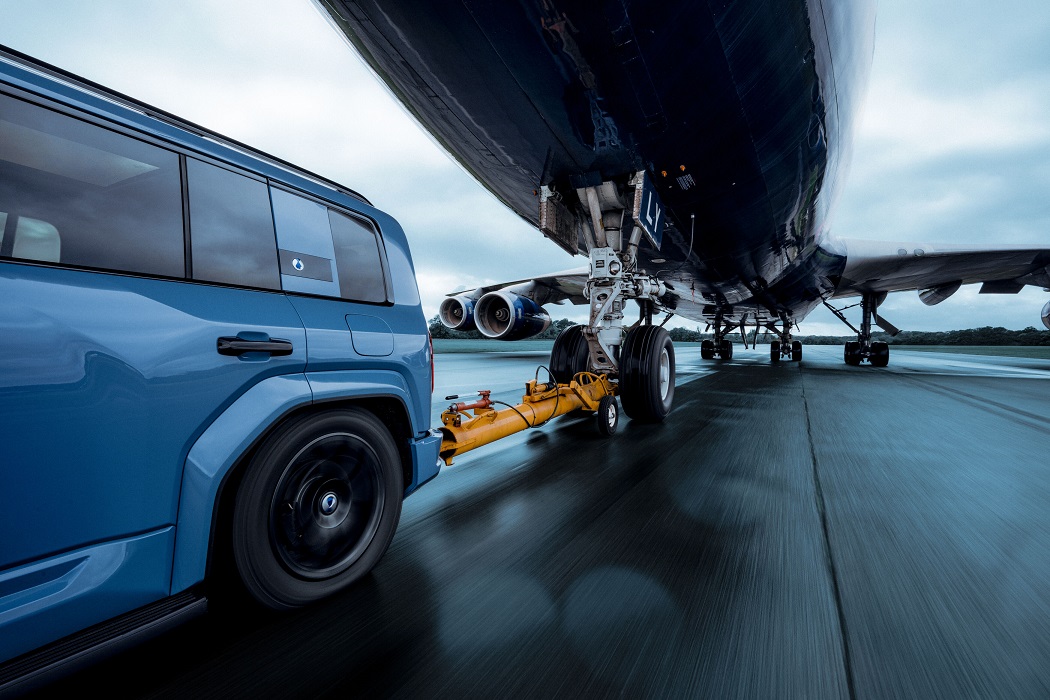
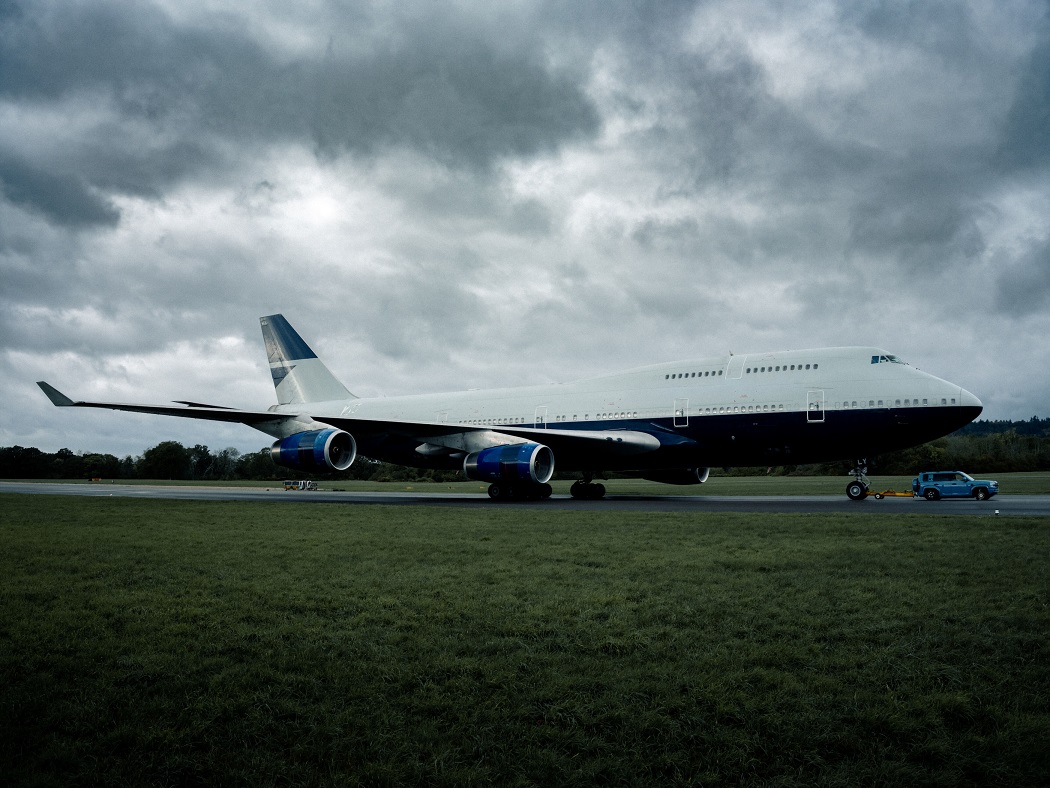
A production-specification BAO 5 in Ultimate trim, lightly modified, performed the runs. A custom towing link joined SUV to aircraft, passenger seating came out to make room for 4,500 kg of ballast in two-wheel mode and 2,000 kg in three-wheel mode, and small axle stabilisers compensated for the removed driven wheels. The DMO powertrain ran in standard form: three electric motors, one per axle plus a generator unit, paired with a 1.5-litre turbocharged petrol engine for 544 PS and 760 Nm. Electric-only range stands at 56 miles, with 537 miles available from a full tank and charge.
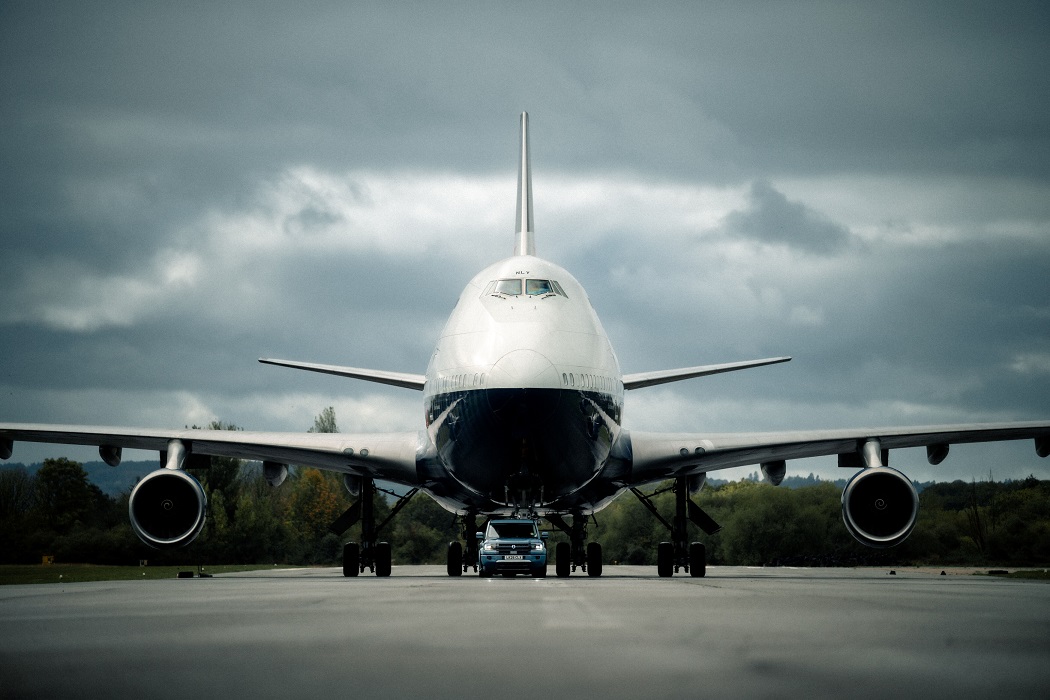
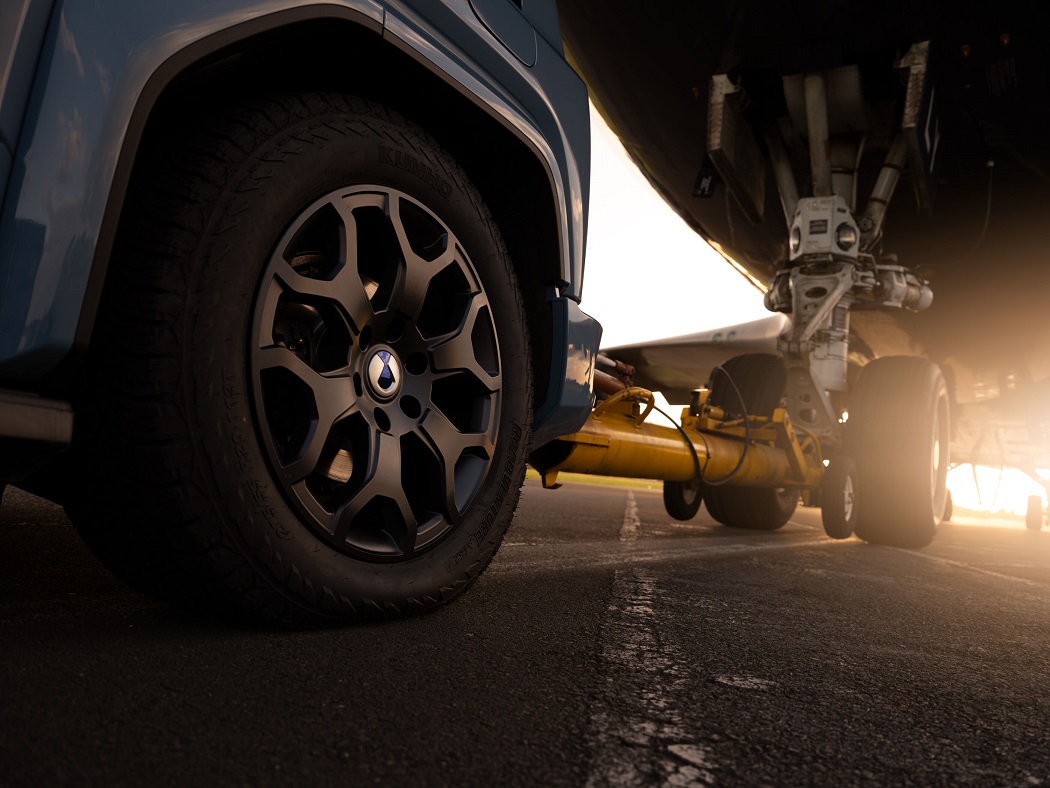
The aircraft, a Boeing 747-400 retired from service in 2020, still carries its engines and furnished interior at roughly 180 tonnes. Early practice runs went smoothly, but torrential rain made the final day far tougher. Once the runway dried enough for traction, the 747 finally moved. Post-run inspections found no stress on the powertrain, chassis or tyres.
Comments (0)
ADD COMMENT